OEM Powder Storage Silo Solutions for Reliable Bulk Handling
2026-11-16
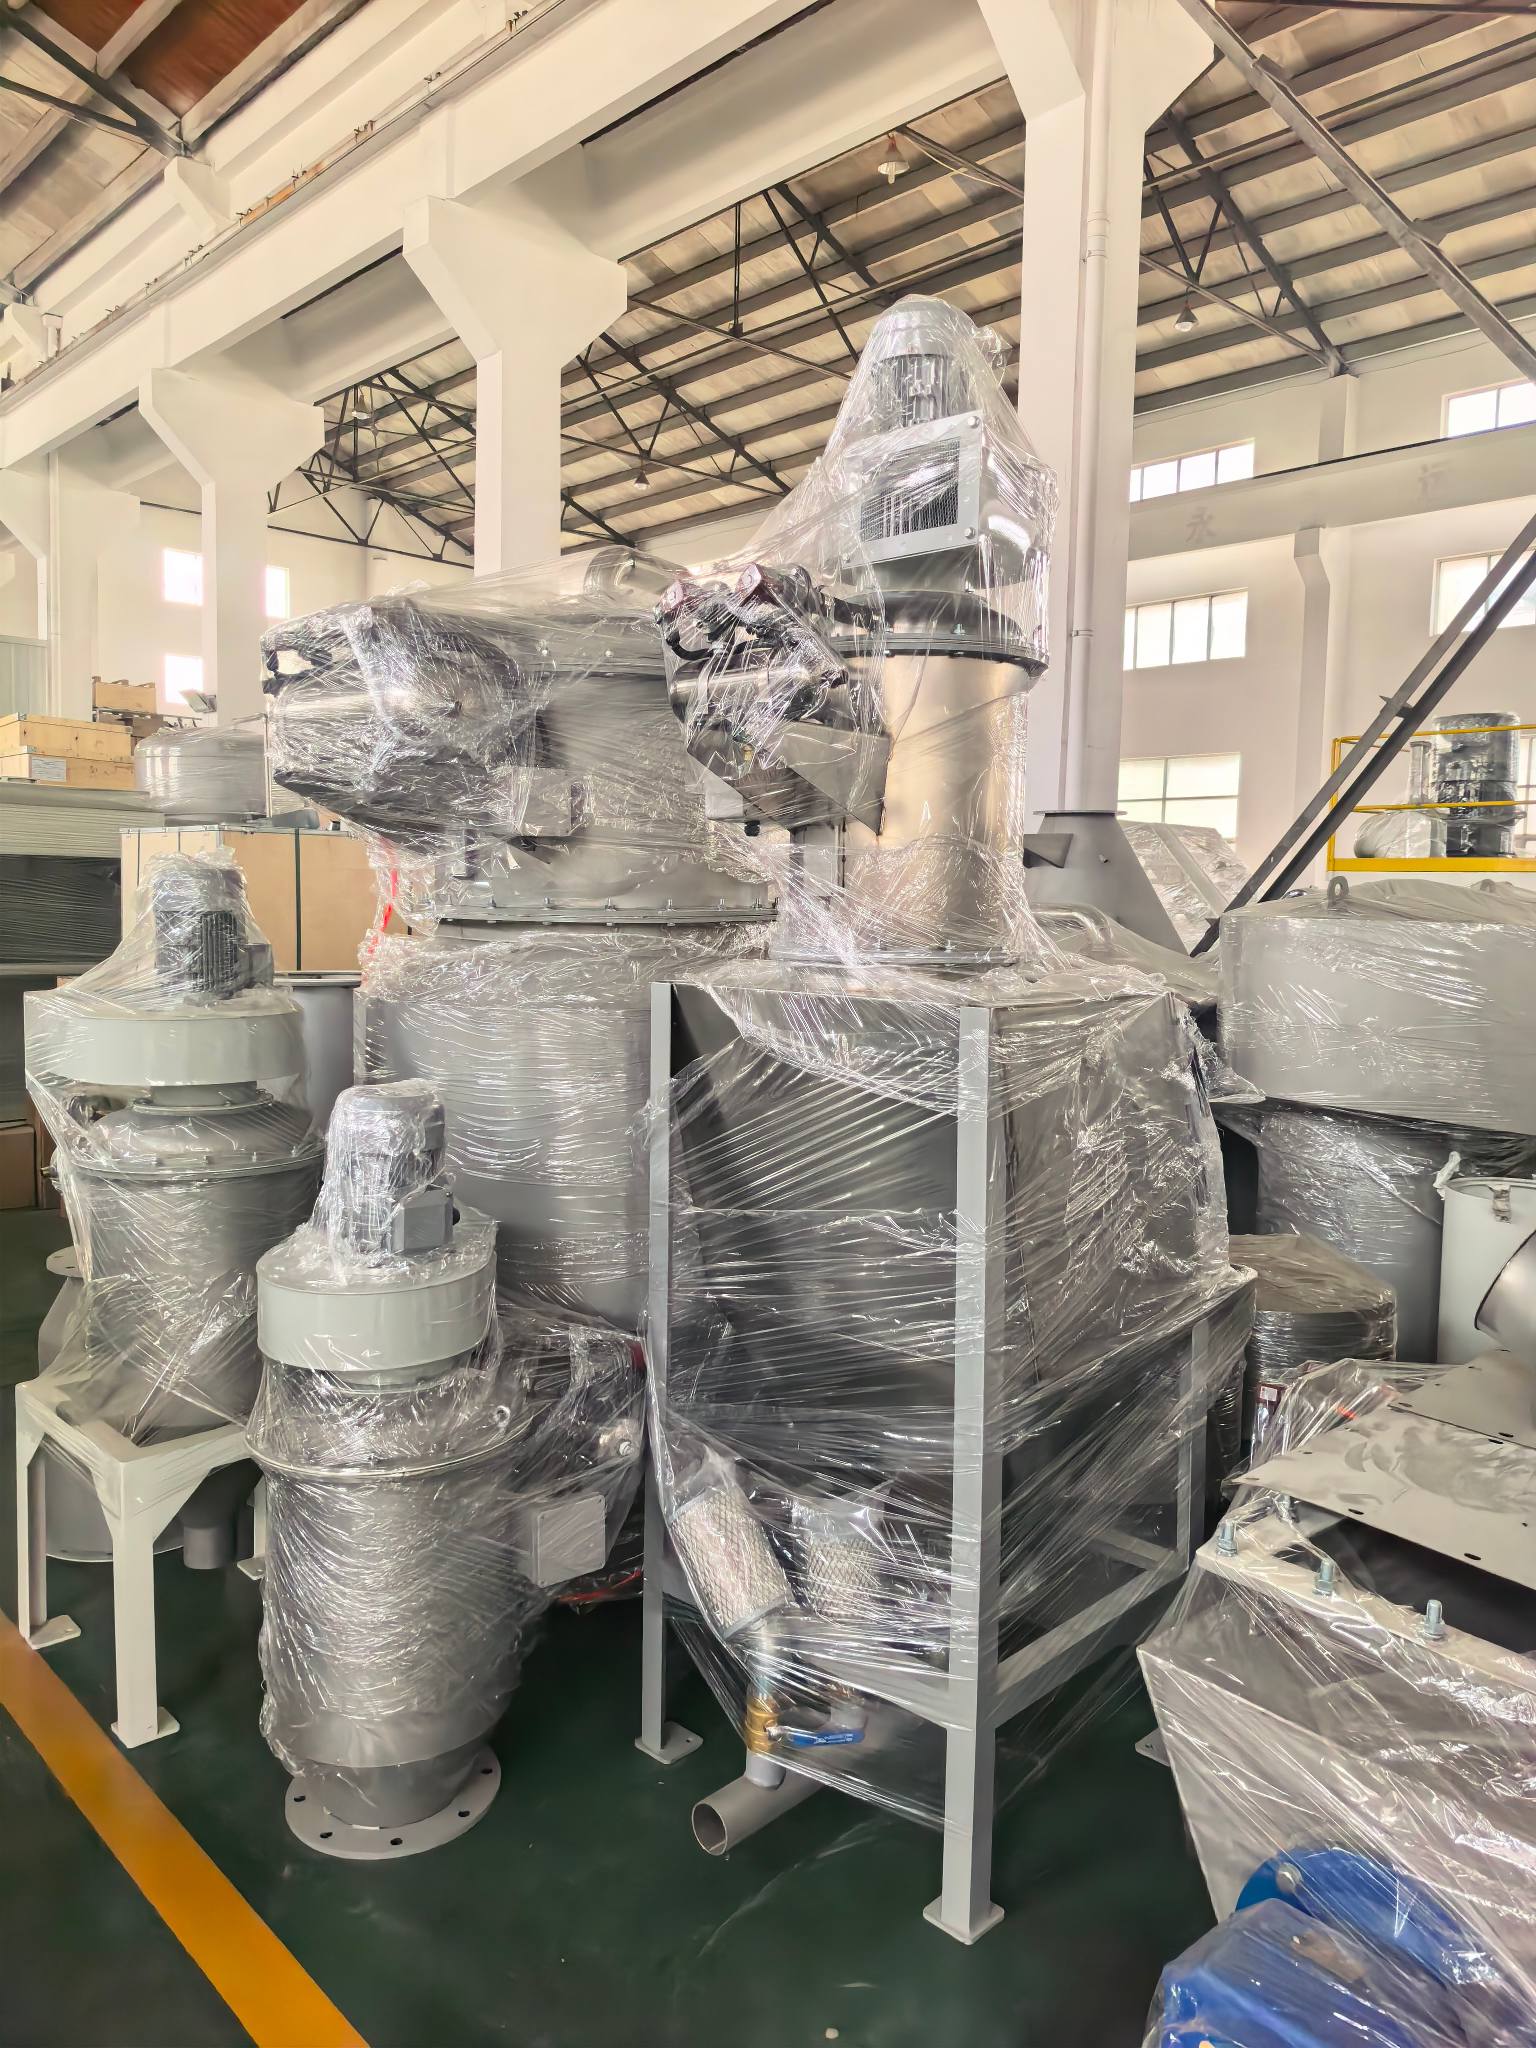
When bulk powders start bridging or segregating inside a generic storage silo, the hidden costs often show up as unplanned downtime and inconsistent feed rates. Reliable bulk handling starts long before discharge, with OEM powder storage silo solutions that match the silo design to the actual flow behavior of your material. Fanchang Machinery approaches these systems with that operational reality in mind, combining sturdy fabrication with attention to discharge dynamics. In this article, we explore what to look for in a powder storage silo and why the right OEM partnership makes a measurable difference.
Why Standard Silo Shapes Struggle With Difficult Powders
Most standard silo geometries are built around the assumption that material will move downward as a single mass once a discharge gate opens. That assumption falls apart with cohesive or sticky powders. Cocoa powder, calcium carbonate, and certain starches can pack tightly under their own weight, forming bridges across the outlet or leaving a stagnant core while only the product above the discharge point empties. The result is a silo that looks half full from the outside but has stopped delivering material at the line.
The problem is often less about the powder itself and more about how wall angles and outlet dimensions interact with its flow properties. Shallow cones and flat bottoms do not create enough shear at the walls to overcome internal friction, so the powder starts to hold itself up. Once moisture or temperature changes cause slight caking, the material gains enough cohesive strength to support a stable arch. Even a hopper angle that looks generous on paper can fail because the outlet is too small relative to the powder's unconfined yield strength, leaving product stuck above the discharge point.
Another overlooked issue is how standard shapes promote segregation and dead zones. With a centre discharge and sloped sidewalls that are too shallow, fines and coarse particles separate during filling and discharge. The coarse fraction may run out first while finer, more cohesive material stays behind, hardens over time, and requires manual cleaning or pneumatic hammering. A shape that works for plastic pellets or grains often turns into a persistent bottleneck when the same geometry is applied to powders with higher fat, moisture, or electrostatic charge.
The Discharge Zone Fix for Bridging and Ratholing
The discharge zone fix reworks how chip movement gets logged when a table is busy, so the small hand-to-hand transfers that used to blur into normal buy-ins are treated as their own events. Bridging and ratholing both depend on the tray looking balanced at the end of a session, and this update drops a clearer boundary between the active betting area, the rack, and the space just off the felt. That change alone makes the quiet chip pass between players or the slow pocketing of green and black chips much harder to hide.
What most floor teams notice first is how much cleaner the reads become during a shift. A player who ratholes tends to remove chips in predictable little steps, while bridging often shows up as two or three people evening out their stacks right after a win. The updated zone logic keeps those moments visible instead of folding them into the background noise of the game. It also cuts down on the review time after a disputed count, because the transaction trail now reflects where the chips physically moved rather than where the system assumed they should have gone.
OEM-Ready Mounting Points That Simplify Line Integration
Most machines leave the factory with a few generic holes and a prayer that they line up with whatever the integrator needs. That approach falls apart on a real line, where someone ends up drilling through powder coat or welding brackets between conveyor sections. OEM-ready mounting points flip that pattern. They are laid out where vision systems, cable trays, sensors, and safety guards naturally belong, so the machine arrives pre-negotiated with its surroundings.
The benefit becomes obvious the first time a station has to move six inches during commissioning. Instead of fabricating adapter plates or calling the OEM for permission to modify a structural member, the team simply unbolts and relocates the module. Because the mounting grid follows the machine’s own frame geometry, accessories tend to land away from doors, heat sources, and washdown zones. It cuts a lot of polite arguments between controls, mechanical, and safety reviewers.
Later, when the line gets rebalanced for a new package size or an inspection step is added, those same bosses and slots remain useful. A retrofit can be attached to the original hard points with standard fasteners and existing drawings, without weakening the frame or violating enclosure ratings. It is the kind of feature nobody notices until it saves them a full day of rework.
Dust-Tight Filling Sequences Built Around Your Current Plant Layout
Rather than asking you to rearrange processing rooms or move bulk storage, the filling sequence is drawn directly over your existing floor plan. Conveyor runs, hoist clearances, mezzanine edges, and even irregular column spacing become fixed points that shape the equipment layout, so the line fits without cutting into adjacent traffic lanes.
Each transfer point from intake to bag or drum filling is enclosed and kept under slight negative pressure. This closes off the routes where fine powder normally escapes—hoppers, scale hoppers, and stitching stations—while still leaving enough access for operators to reach spouts, swap rolls, and clear jams quickly.
Because the sequence follows the plant as it stands, installation usually happens in short windows between production runs. You keep the quirks of the building, but lose the dust that used to settle on beams, electrical cabinets, and finished packaging nearby.
Liners and Coatings Chosen for the Actual Powder, Not the Datasheet
A datasheet will tell you the median particle size and maybe a moisture spec, but it rarely captures how a powder behaves after it has been sitting in a silo for three weeks or moving through a transfer line at 2 a.m. We choose liners and coatings by running the actual material through the actual conditions: angle of repose tests, abrasion coupons, humidity exposure, even electrostatic checks when fines are present. The same grade of calcium carbonate from two suppliers can wear a stainless elbow completely differently, and no PDF is going to reveal that.
That is why we treat the powder as the final authority. If a sample builds up on a smooth surface, we look at non-stick coatings or polished welds. If it scratches a hardened plate, we move toward ceramic or tungsten options. The choice gets tied to what the material does when it is slightly damp, slightly warm, or loaded faster than the datasheet assumes.
Sometimes the mismatch is small but expensive: a liner selected from nominal flow data fails after a few months because the real powder has a bimodal distribution and packs harder under pressure. Testing the actual powder costs a little time up front and saves a lot of unplanned downtime later.
Modular Contact Parts That Turn Changeovers Into Hours
Swapping out contact parts can eat up an entire shift if the design forces you to dismantle half the machine. Modular contact parts turn that chore into a quick, tool-free swap. Instead of loosening bolts, unwiring terminals, and hoping the alignment is still right, technicians pull out a worn block and click in a fresh one. The savings show up immediately: changeovers that used to take hours now wrap up in minutes, and the line barely stops moving.
The real advantage comes from how the pieces are split. Wear concentrates on the contact tips and arc chutes, but the housing, springs, and mounting rails rarely need attention. Modular construction lets you replace only the consumed section while leaving the rest untouched. That means fewer spare parts to stock, less chance of misassembly, and a maintenance routine that feels more like reloading a cartridge than rebuilding a switch.
Plants with frequent product swaps notice the difference fast. A modular contact set can be preloaded with different ratings or materials, so switching from a high-current run to a low-current run is just a matter of changing the block. Downtime drops from hours to the length of a coffee break, and operators don't need a specialist standing by. It's not just a design tweak; it's a way to keep production fluid when every minute counts.
FAQ
An OEM silo is built around a specific material and process flow rather than forcing a process to fit a fixed design. Elements such as hopper angle, outlet sizing, liner selection, and discharge aids are matched to the powder's shear properties and the downstream equipment. That approach tends to reduce bridging, segregation, and downtime that generic silos often create.
It depends on what is being stored and how the site is managed. Welded construction offers fewer crevices and easier cleaning for moisture-sensitive or cross-contamination-prone powders. Bolted panels can shorten installation time and lower freight costs for large capacities, but they need careful gasketing and surface finishing to avoid product hang-up at joints.
The hopper shape and wall angle are the starting point, but wall surface finish and a properly sized discharge opening matter just as much. For difficult materials, options such as air pads, vibratory dischargers, mechanical agitation, or fluidizing cones can be added. The key is selecting these based on measured flow properties instead of guessing from bulk density alone.
It is possible, but only within limits. A silo designed for a free-flowing granule may not reliably discharge a cohesive or fatty powder. If multiple materials must share a vessel, the design usually has to compromise on hopper geometry or include adjustable discharge aids. It is generally safer to group powders with similar flow behavior and abrasive or moisture properties.
For abrasive service, carbon steel with a durable internal lining or wear-resistant plates in high-impact zones is common. For corrosive or ultrapure applications, stainless steel such as 304 or 316 is often used, sometimes with electropolishing or coatings to reduce adhesion. The liner also needs to remain compatible with cleaning chemicals and temperature swings.
Filling needs a vent path that lets displaced air escape without carrying powder out. That usually means a properly sized bin vent filter or central dust collection line, along with level sensors that stop the fill before the filter is submerged. Some systems also use a fill pipe designed to reduce free-fall and minimize dust generation at the start of loading.
Beyond total capacity and available footprint, you need the powder's bulk density, particle size range, moisture content, flow function, abrasiveness, and temperature at filling and storage. Discharge rate, downstream feed requirements, headroom, and cleaning method also drive the design. The more complete the powder data, the fewer field adjustments are usually required.
The best designs reduce horizontal ledges, sharp corners, and inaccessible seams from the start. Large access doors, rinse ports, and polished internal surfaces make manual cleaning or CIP easier. For frequent changeover, a dedicated silo per product family avoids cross-contamination risk, while quick-release filters and discharge components shorten turnaround time.
Conclusion
Powder storage rarely fails because the vessel is too small; it fails because standard hopper angles and outlet geometry assume a material that flows like the datasheet says it should. When the powder is cohesive, fatty, or prone to settling, conical sections create stable arches and narrow rat holes that starve downstream equipment. The fix is not a universal steeper cone. It is a discharge zone matched to the powder’s actual shear behavior, with transition angles, enlarged outlets, and controlled vibration or fluidization only where the material needs it. OEM mounting features then let the silo drop into an existing line without field-drilled brackets or awkward adapter plates, keeping load paths and sensor positions predictable.
Filling sequences matter just as much as discharge. Dust-tight connections and vented, staged filling can be arranged around the current plant layout instead of forcing a new floor plan. Liners and coatings are selected from powder trials, not generic compatibility tables, so abrasive wear, moisture pickup, or chemical adhesion are addressed before they become downtime. Because contact parts are modular, a product changeover becomes a shift-level task: swap the outlet section, screw, or seal kit and return to service in hours rather than days. The result is bulk storage that handles the powder you actually have, while still fitting the line you already operate.
Contact Us
Contact Person: Darye WANG
Email: [email protected]
Tel/WhatsApp: 86-13501017897
Website: https://www.fcntd.com/